Hey everyone, I’m Jake, and I’ve spent the last 8 years troubleshooting, tweaking, and selling industrial demineralized water systems (you know, the DM plants) to all kinds of manufacturers—from the guys making cleaning supplies to pharma clients who can’t afford to cut corners. Today, I wanna break down one question I get more than any other: “What the hell is our DM water even used for in pharma? I thought it was just for batteries or something.” Fair question. Let’s dive in, no corporate jargon, promise. First, let’s get one thing straight: pharma isn’t like making a bottle of soda or a bag of cereal. If your water’s got even a tiny amount of extra stuff—like calcium, magnesium, sodium, or random heavy metals—you don’t just get a bad taste. You get a failed batch, FDA red flags, and, worst of all, a product that could hurt people. DM water is demineralized, meaning we stripped out almost every single ion that isn’t H2O using resins in our plants—think of it like super purified, no extra “ingredients” that weren’t meant to be there. Let’s start with the stuff you hear about every day: injectables. Like, actual needles, stuff you shoot straight into someone’s bloodstream. I’ve heard pharma clients test regular tap water once, back when they were cutting corners, and found 0.2 ppm of iron in it. That’s not a lot for a fish tank, but for an IV solution? It would react with the active pharmaceutical ingredient (API) and turn the solution cloudy. Cloudy IV fluid means you can’t use it—entire batch wasted, like $50k down the drain. DM water for injectables isn’t just demineralized, it’s often even polished a step further (we call it “water for injection,” WFI, but the base starts with our DM plant). Another big one: oral meds. Sure, you’re swallowing them, not injecting, but water carries the API, excipients, all the other stuff that makes a pill work. If your water has hard water minerals (calcium is the big culprit here), they can bind to the API and make it so the pill doesn’t dissolve when it’s supposed to. That leads to either the pill not working at all or releasing too much of the drug at once—bad for safety. I had a customer last year making blood pressure pills, and they switched to our DM plant, fixed their dissolution rate from 62% to 98% overnight. No more rejected batches, no more rushing to rework production. What about topical meds? Creams, ointments, eye drops. Eye drops are super sensitive—your eyeball hates random minerals. If your DM water has any residual sodium or chloride, it’ll burn like crazy, and worse, it can mess up the pH balance of the eye, leading to irritation or even mild infections. I remember a small eye care startup I worked with a couple years back; they were using distilled water before, but it couldn’t keep up with their production volume. Our DM plant handled 10,000 liters an hour, no problem, and their eye drop batch pass rate went from 85% to 99% in three months. Beyond the actual drugs themselves, DM water is everywhere in the pharma manufacturing process. We’re talking equipment cleaning. When you switch from making one drug to another, you have to clean every pipe, reactor, mixer, everything. Tap water with minerals leaves scale on equipment—scale builds up over time, makes machines less efficient, and can flake off into the next batch. We had a client who ran their production equipment for 6 months without using DM water for cleaning, and they had to replace a $120k reactor because of mineral build-up. That’s way more than the cost of a DM plant, right? Also, formulation tanks, mixing vessels, even the water used to make the packaging (like blister packs for pills) needs to be DM water—you don’t want leftover chemicals from packaging mixing with your product. Wait, and what about biotech? That’s the stuff with living cells, right? Monoclonal antibodies, vaccines, all that. Cells are delicate—they live in a specific environment, and even a tiny amount of mineral ion can throw off their growth. DM water is the base for cell culture media. If your water has high conductivity (which means lots of minerals), it’s toxic to the cells. I worked with a biotech firm developing a COVID booster a couple years ago (yeah, back in 2021, that was wild), and their old DM plant was only removing 99% of ions. We upgraded their system to a mixed-bed resin polish step, and their cell viability jumped 20%—meaning they didn’t have to use more raw materials, and they got more product out of every run. That’s huge when you’re racing to get a vaccine to market. Let’s talk about quality control, too. Pharma companies have to test every batch of water, every single day, to make sure it meets USP standards (that’s the U.S. pharmacopeia, basically the rulebook for pharma stuff). Our DM plants are designed to hit those standards consistently—no surprises, no last-minute fails. A lot of small pharma companies think they can get away with cheaper water, like reverse osmosis (RO) water, but RO only removes about 95-99% of ions, not 99.9% like DM. RO works for some things, but pharma needs that extra step. I’ve had so many clients come to me after wasting tens of thousands of dollars on RO batches that got rejected, saying “why didn’t you tell me this earlier?” Because I don’t sell hype, I sell actual results. Also, maintenance for DM plants is way simpler than most people think. We design our systems so they can be maintained by regular plant staff, no fancy PhD required. Resin replacement is every 12-18 months, and we send a technician to do it if they want, or walk them through it over a call. No downtime, no huge costs. Wait, let’s address a common myth: people say “distilled water is the same as DM water.” Distilled is made by boiling water and condensing the steam, and it removes most minerals, but it’s not consistent. Distilled water can have volatile organic compounds (VOCs) that DM plants catch, and it’s not scalable for large production runs. You can’t make 100,000 liters of distilled water an hour for a big pharma plant—you’d go broke on energy costs. DM plants are built for volume, consistent purity, and lower long-term costs. Let’s get real about the bottom line, too. Pharma margins are tight, but a rejected batch can wipe out a month’s profit. I had a client last year that had a $200k batch of diabetes drug rejected because their water had too much calcium. They were using an old DM plant that was failing. We installed our system in 3 days, and their next batch passed inspection with zero issues. That’s not just fixing a problem, that’s saving a business. Another point: regulatory compliance. The FDA, EMA, all the big pharma regulators require documentation of your water purity. Our DM plants track every single reading—conductivity, ion levels, everything—and store data so you can prove you’re meeting standards, no gaps, no headaches. No more staying up till 2 a.m. trying to write a compliance report because your old system didn’t log data. For smaller pharma startups, this is huge—when you’re trying to get your product approved, you can’t have any gaps in your process, and water purity is one of the first things auditors check. I’ve helped three different startups get through FDA audits just by showing them how to set up their DM plant correctly. Now, I know some people reading this might be thinking “we already have a water system, why would we switch?” Maybe your old DM plant is old, or it’s not handling your volume as you grow, or you’re having more fails than you should. That’s why I’m here. I don’t pressure anyone to buy, but I’ve seen too many companies get stuck with a system that doesn’t keep up as their pharma operation scales. Whether you’re making a niche topical cream or a huge biologic drug, DM water from a properly designed industrial plant isn’t a luxury—it’s a necessity. Let’s wrap this up: when you’re working in pharma, every little part of your process matters, and water is the foundation. DM water isn’t just “pure water”—it’s the difference between a safe, effective product and a rejected batch, a regulatory fine, or worse, harming patients. I’ve been doing this long enough to know that cutting corners on water is the worst call you can make. If you’re a pharma professional dealing with water purity issues, or you’re looking to set up a new DM plant for your operation, hit me up. No sales pitch, just straight talk about what your specific facility needs. Let’s work out a solution that fits your production volume, your budget, and most importantly, keeps your products safe and compliant. Industrial dm Plant

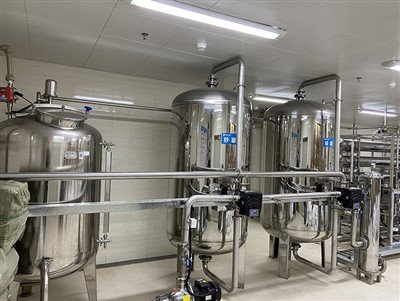
Ultra Pure Water System References
- U.S. Pharmacopeial Convention. (2023). General Chapter <1231> Water for Pharmaceutical Purposes.
- International Council for Harmonisation of Technical Requirements for Pharmaceuticals for Human Use. (2022). Q7 Good Manufacturing Guide for Active Pharmaceutical Ingredients.
- European Directorate for the Quality of Medicines & HealthCare. (2021). Ph.Eur. 10th Edition: Monograph 0169 Purified Water.
- American Society of Mechanical Engineers. (2020). Design Guidelines for Industrial Water Treatment Systems for Pharmaceutical Manufacturing.
Shenzhen Jkon Environmental Protection Technology Co., Ltd.
As one of the most professional industrial dm plant manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy customized industrial dm plant made in China here from our factory. Contact us for more details.
Address: Shanghenglang Industrial park, Daloang Street, Longhua District, Shenzhen, China
E-mail: sales@jkontech.com
WebSite: https://www.jkontech.com/
